When a shop comes to me looking for cast parts, they’re not just hunting for metal pieces that fit a blueprint—they’re hunting for consistency, reliability, and a part that won’t fail when it’s bolted into a $100,000 machine or a critical agricultural tractor that feeds a family. For 12 years, I’ve run a small, family-owned cast parts supplier, and early on, I made the mistake of turning out a batch that was “close enough” to spec to save 30 minutes of extra work. That batch cracked during stress testing, cost the client a $20,000 production shutdown, and taught me a lesson I carry with me every day: national quality standards for cast parts aren’t just paperwork—they’re the backbone that keeps suppliers, manufacturers, and end users all safe and profitable. Cast Parts
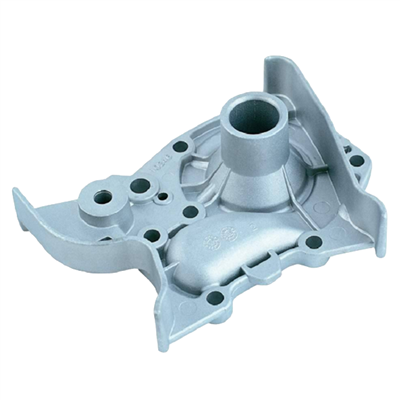
If you’re new to sourcing cast parts, the jargon around these standards can feel like being handed a book in a second language. But let’s break it down simply, through the lens of what we actually use in our shop every day. First, in the U.S. (one of the largest markets for cast parts), the primary standard we rely on is ASTM International’s cast metal standards—specifically ASTM A for ferrous castings, which covers everything from iron to steel, and ASTM B for non-ferrous castings like aluminum and brass. Then there’s SAE International, which works hand in hand with ASTM, focusing on automotive and aerospace cast parts, the two sectors where part failure can have life-threatening consequences.
Let’s start with the foundational requirements that apply to every single cast part, no matter the material. First is chemical composition. Cast parts are only as good as the mix of metals we melt down. For example, if we’re making gray iron for engine blocks (one of our most common orders), ASTM A48 sets exact limits for carbon, silicon, manganese, and trace elements like sulfur. Too much sulfur, and the iron becomes brittle; too little, and it won’t machine cleanly. Early in my career, a new employee accidentally added an extra 0.2% sulfur to a batch of gray iron valve bodies. We caught it before shipping, but it meant melting 1,200 pounds of metal down and starting over—cost us $800 in material and a missed delivery window, but saved us from the call we would have gotten when those valve bodies cracked in a customer’s engine. ASTM doesn’t just pull these numbers out of thin air—they’re the result of decades of testing to ensure the metal behaves predictably under heat, pressure, and wear.
Next is dimensional accuracy, which is probably the most visible part of any quality check. A cast part that’s supposed to fit a 2-inch bolt hole that’s actually 2 and 1/16 inches might seem trivial, but when you’re assembling a line of 1,000 tractors a day, that extra 1/16 of an inch means 100 minutes of extra labor adjusting each part, plus a higher risk of leaks or misalignment. For dimensional tolerances, we rely on ASTM A802, the standard for dimensional tolerances for ferrous castings. This standard breaks down tolerances by casting size: a small 1-inch bracket gets a tolerance of ±0.005 inches, while a large 2-foot gear housing gets ±0.020 inches. We use a coordinate measuring machine (CMM) in our shop to check every critical dimension on high-volume orders, and even for smaller jobs, we use calipers and gauges to make sure we’re within spec. I’ve had clients come to us after working with another supplier whose parts were consistently off by 0.015 inches on a 1-inch hole—enough that they were throwing out 10% of parts during assembly, which was eating into their margins. Once they switched to our shop, where we stick to ASTM A802 tolerances, that scrap rate dropped to less than 1%.
Then there’s surface quality, which is often overlooked but just as important. A cast part’s surface isn’t just about looks—it affects how it machines, how it seals, and how it resists corrosion. For example, a cast pump housing with a rough interior surface will cause turbulence in the fluid it carries, leading to higher energy use and faster wear on the pump. ASTM A126 sets standards for surface roughness on cast iron parts, requiring that critical sealing surfaces have a maximum roughness of 125 microinches, while non-critical surfaces can be up to 250 microinches. We also use magnetic particle inspection (MPI) for ferrous cast parts and liquid penetrant inspection (LPI) for non-ferrous parts to find tiny surface cracks or porosity that would be invisible to the naked eye. Last year, we had a batch of aluminum castings for a forklift mast that showed a small, 1mm surface crack during LPI—without that check, the crack would have grown over time, leading to a forklift tipping at a warehouse. That’s not a risk we’re willing to take.
Beyond these basic checks, there are standards tailored to specific industries, and that’s where most of our repeat business comes in. For automotive cast parts, SAE J431 is the go-to standard for gray iron castings, which is stricter than the basic ASTM A48. SAE J431 requires higher tensile strength and hardness to handle the repeated stress of engine cycles. For agricultural cast parts, which have to survive dirt, moisture, and extreme temperatures, ASTM A536 for ductile iron castings sets requirements for impact toughness, so a plowshare won’t snap when hitting a rock in a field. For aerospace cast parts, which are held to the highest standards, AS9100 (the quality management system for aerospace) requires traceability for every step of the casting process—from the raw metal batch number to the inspector who signed off on the final part. That means if a part ever fails, we can pull the entire production history, which is non-negotiable for that industry.
Wait, but what about smaller suppliers? Do these standards apply to everyone? The short answer is yes, and it’s one of the things I tell other small suppliers when they come to me asking for advice. Early on, I thought that meeting basic ASTM standards was enough, but I soon learned that clients don’t just want us to meet the minimum—they want us to document that we meet the standards. So we keep detailed records: chemical test reports from every melt, CMM reports for every critical dimension, inspection logs for every batch. That’s not just red tape—it’s how we build trust with our clients. Last year, a startup company making electric delivery trucks needed a supplier for their brake caliper castings, and they turned down a larger supplier who quoted a lower price because that supplier couldn’t provide full documentation of their ASTM compliance. They chose us instead, and that order turned into a long-term contract that’s now 30% of our business.
I also want to address a common misconception I hear all the time: that these standards make cast parts more expensive. Sure, we have to invest in testing equipment, train our team, and waste some material when a batch doesn’t meet spec. But when you add it up, that cost is nothing compared to the cost of a recall, a production shutdown, or a client losing their reputation. A few years ago, I heard about a large casting supplier that skipped a critical inspection for a batch of steel crane hooks, and one of those hooks failed at a construction site, killing a worker. The supplier was forced to pay millions in damages and lost all their major construction clients. That’s the real cost of cutting corners on national quality standards.
For any manufacturer sourcing cast parts, the key is to ask questions: Do you provide full documentation of ASTM compliance? What inspection methods do you use for critical defects? Can you adjust to industry-specific standards for my application? A good supplier will be able to answer those questions clearly, and if they can’t, that’s a red flag. For us, we don’t just see our parts as metal castings—we see them as a vital part of whatever machine or product our client is building, and that means holding ourselves to the highest national standards, every single time.
At the end of the day, national quality standards for cast parts are there to protect everyone: the supplier, who doesn’t want to face liability for a bad part; the manufacturer, who doesn’t want to lose time and money from defects; and the end user, who relies on the product to be safe and reliable. As a cast parts supplier, my job isn’t just to melt metal and pour it into a mold—it’s to deliver parts that people can trust, and that starts with following those standards, every step of the way. If you’re looking for a cast parts partner that’s serious about quality, compliant with all relevant national standards, and has the track record to prove it, we’re ready to talk. Whether you need a small batch of custom parts or high-volume production for an ongoing project, we can work with you to meet your exact requirements without cutting corners.
Automotive Turned Parts References
ASTM A48, Standard Specification for Gray Iron Castings
ASTM A802, Standard Practice for Dimensional Tolerances for Ferrous Castings
ASTM A126, Standard Specification for Gray Iron Castings for Valves, Flanges, and Fittings and Other Piping Components
ASTM A536, Standard Specification for Ductile Iron Castings
SAE J431, Gray Iron Castings for Automotive Applications
AS9100, Aerospace Quality Management System Requirements
Hangzhou Zhalihui Import And Export Co., Ltd.
We are one of the most experienced cast parts manufacturers and suppliers in China, specialized in providing high quality customized products. Please feel free to buy discount cast parts in stock here from our factory. Contact us for quotation.
Address: Room 2801, Building 2, Taifu Plaza, No.17, Tonghui Middle Road, Chengxiang Street, Xiaoshan, Hangzhou, Zhejiang
E-mail: Chars_1979@hotmail.com
WebSite: https://www.zhalihui.com/
